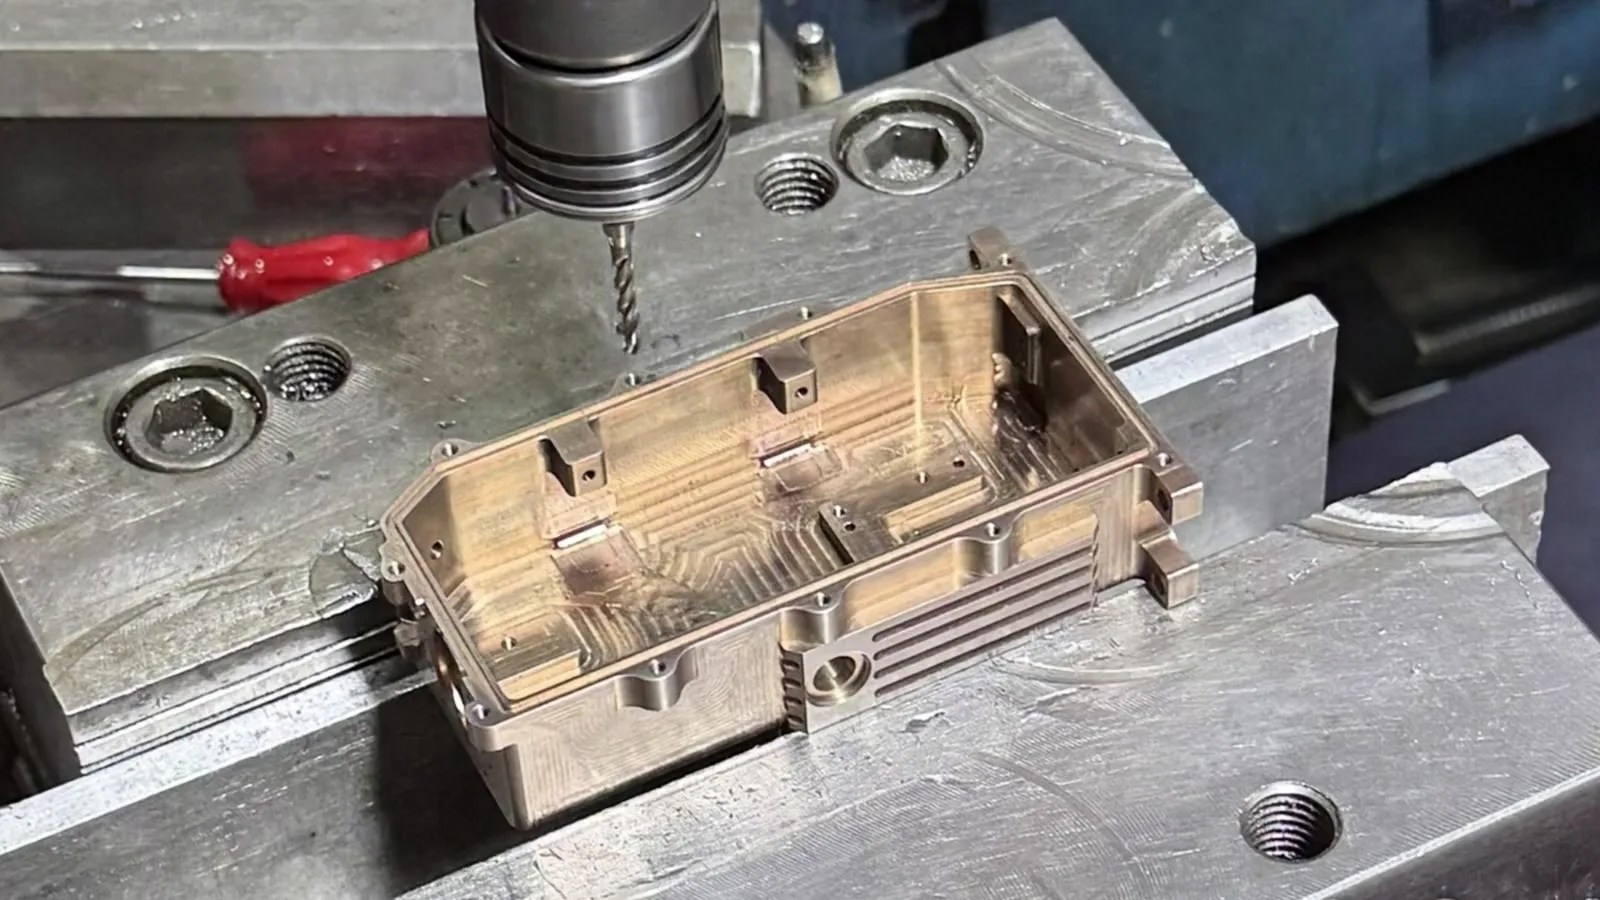
Threads that fit
the first time.
Tapped holes and cut threads — metric, UNC, UNF, ACME and custom forms, internal and external.
Threads are often the feature that decides whether a part works. We tap holes and cut internal and external threads on our lathes and machining centers — standard or custom forms — and gauge every one before the part ships.
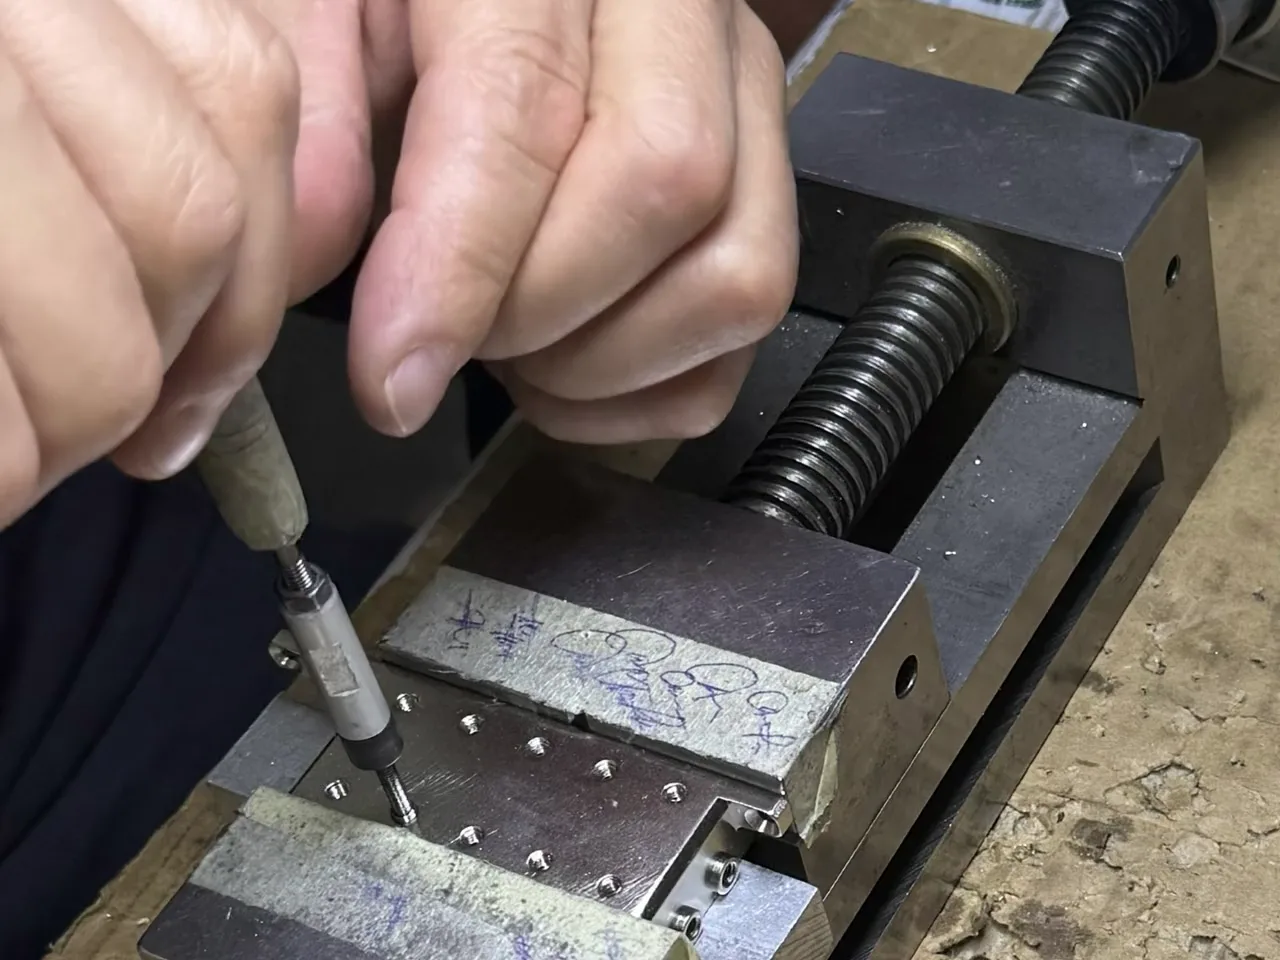
Tapped holes, done right.
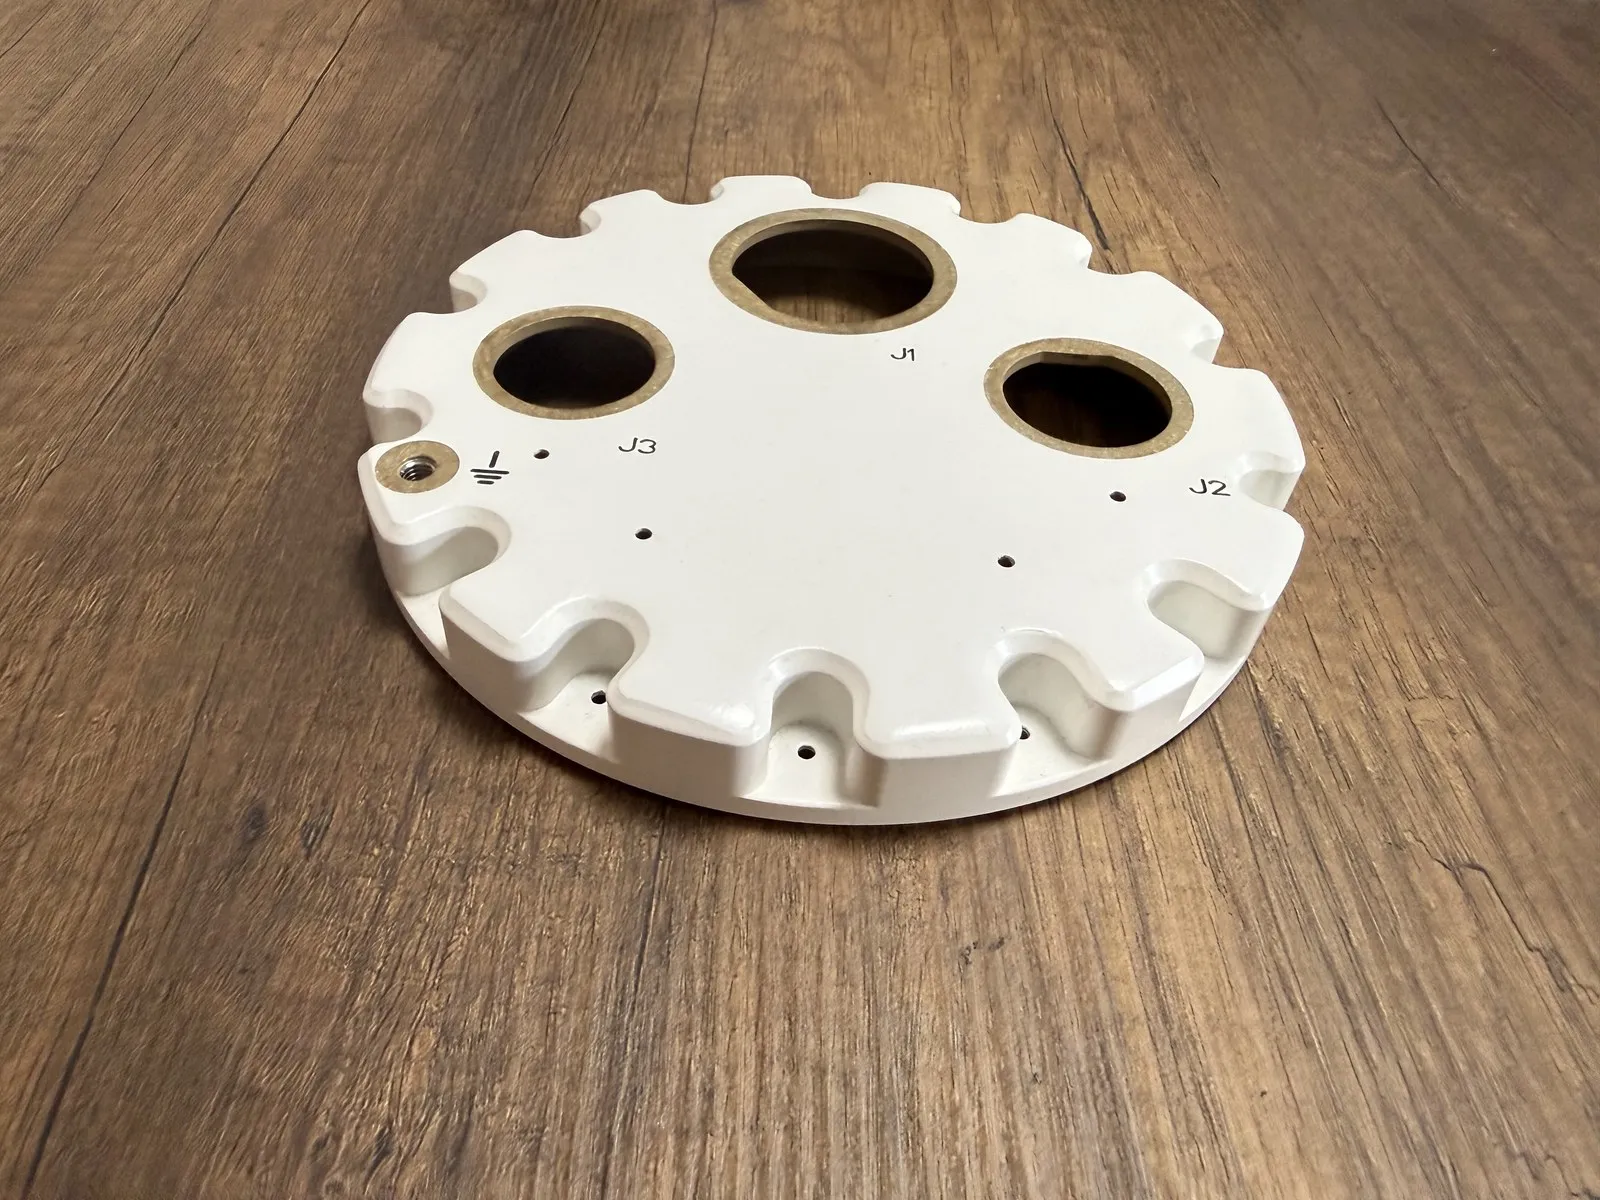
Blind and through tapped holes in every material we machine — with thread milling for large, deep or critical threads where a tap isn’t the best tool.
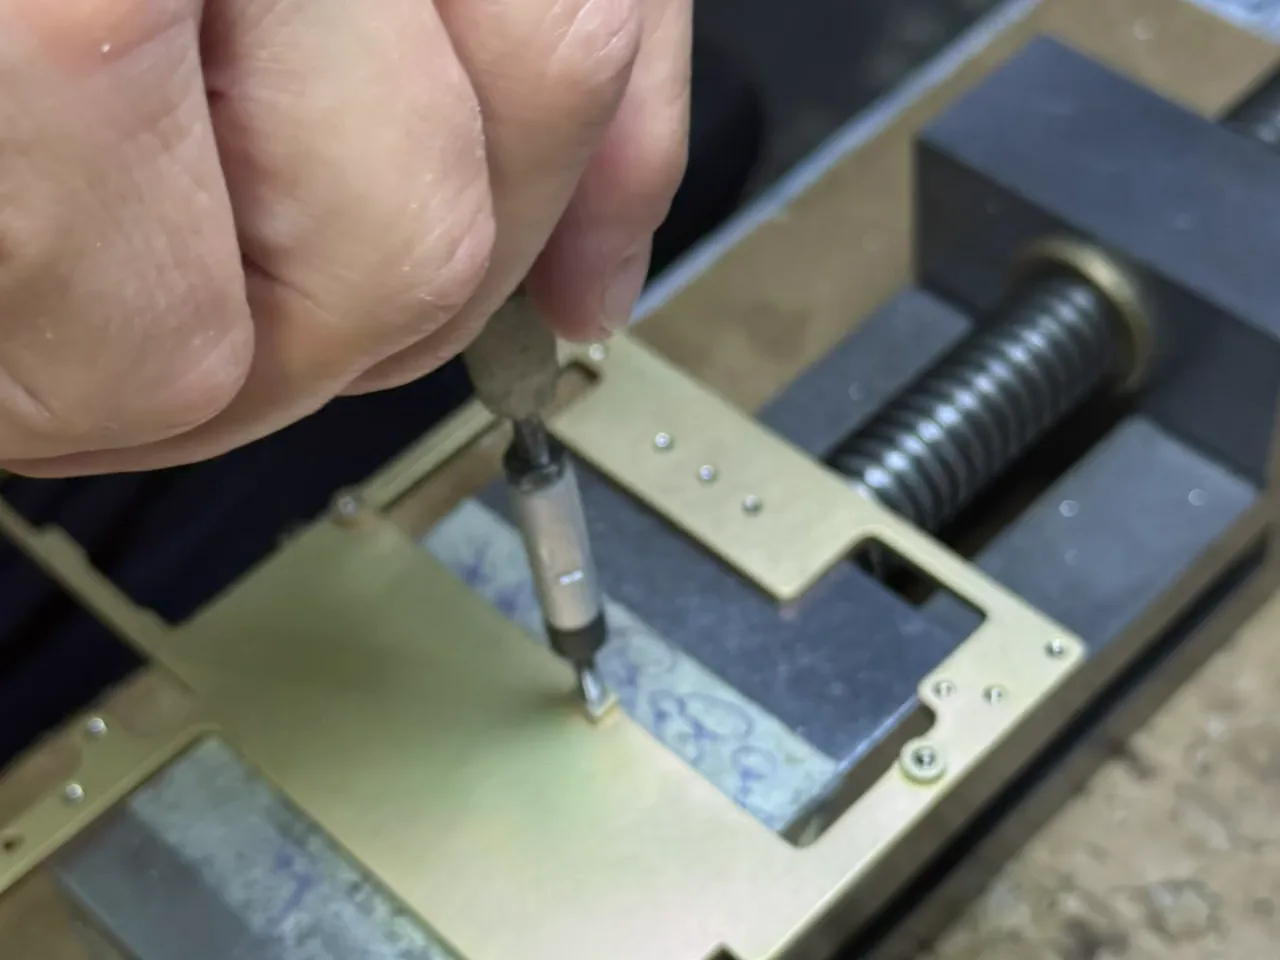
Standard and custom forms.
Metric, UNC, UNF and ACME threads as well as custom profiles — single-point turned or milled, depending on the part.
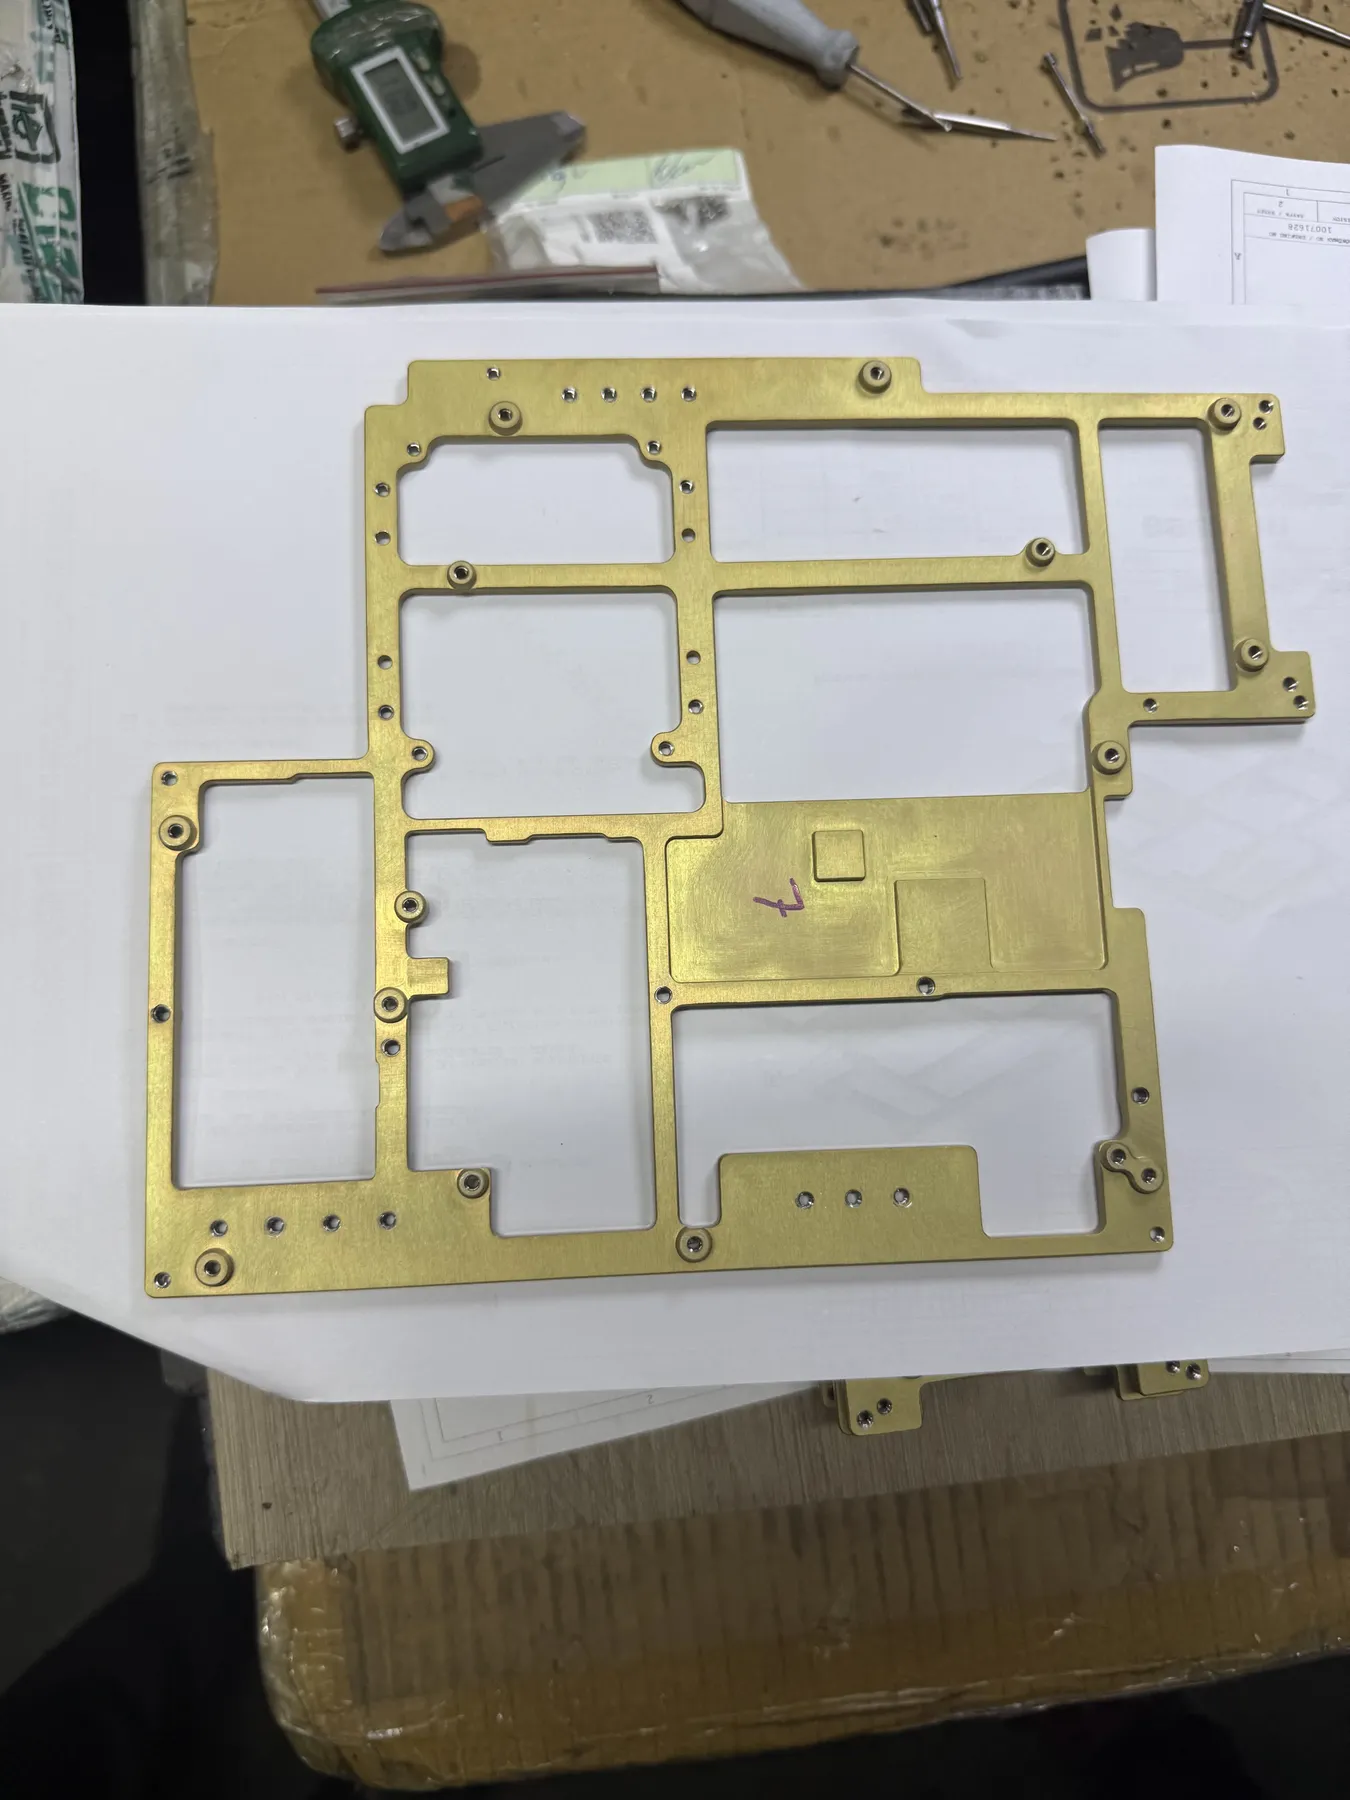
Gauged, not guessed.
Every thread is checked with go/no-go gauges before shipping, so it assembles on the first try.
- Tapped holes & patterns
- Threaded shafts & studs
- Fittings & adapters
- Lead screws (ACME)
- Thread inserts
- Custom fasteners
- Steel 1018 / 4140 / 4340
- Stainless 303 / 304 / 316
- Aluminum 6061 / 7075
- Brass 360 / 385
- Bronze 932 / 954
- Plastics
Threading & tapping questions.
Which thread types can you cut?
Metric, UNC, UNF and ACME threads, plus custom thread forms — both internal and external, including tapped blind and through holes.
Do you check every thread?
Yes. Every thread is gauged before the part ships.
Can you re-cut threads on an existing part?
Send us a description or photo of the part and we’ll let you know.
Have a drawing?
Send it over — we’ll reply with a price and lead time, usually within one business day.
Request a quote →